
Account for pan diameter and material in high-load commercial kitchens
In high-volume restaurants, hotel kitchens, central commissaries, and catering operations, an incorrectly matched burner can create three costly problems: slow recovery, unstable cooking temperatures, and unnecessary fuel consumption. A 300 mm pan does not absorb heat like a 600 mm stockpot, while stainless steel, aluminum, cast iron, and multilayer cookware transfer heat at very different rates. The challenge becomes more serious in high-ambient-temperature kitchens, high-humidity coastal environments, or installations with low gas pressure and limited electrical capacity. If commercial range burner power is selected only by nominal BTU output, the operator may experience excessive flame around a small pan or insufficient recovery under a large load. The result is wasted energy, longer cooking cycles, and inconsistent food quality.
For professional cooking lines, 100–130 mm burners commonly suit 180–300 mm pans, while 150–180 mm high-output burners are better for 300–450 mm cookware. A practical design target is 60–75% useful heat transfer to the pan, with stable combustion and sufficient recovery capacity under the actual operating load.
Retailers, importers, wholesalers, and distributors can continue below to examine practical sizing methods, operating conditions, and representative engineering cases. The following solutions show how a professional Manufacturer and Supplier can adapt burner performance to real commercial cooking environments.
Estimate useful heat at the cooking surface
Nominal burner output is only the starting point. For an engineer, the important value is the heat that actually reaches the cookware. A 100,000 BTU/h burner does not automatically deliver 100,000 BTU/h into a pan. Heat is lost through combustion exhaust, radiation, convection, gaps between the flame and pan, and poor flame-to-pan geometry. This is why gas burner heat transfer must be considered together with pan diameter, material, bottom thickness, liquid volume, and operating time.
For a typical commercial range, a useful preliminary calculation is:
- Burner input: 60,000–120,000 BTU/h for general restaurant cooking.
- Estimated useful pan-side heat: approximately 60–75% under well-matched conditions.
- Small sauce pan diameter: approximately 180–240 mm.
- Medium sauté or boiling pan diameter: approximately 240–320 mm.
- Large stockpot or wok support diameter: approximately 320–450 mm or more.
- Target flame pattern: concentrated beneath the cookware base rather than extending substantially beyond its perimeter.
For example, a 90,000 BTU/h burner operating at 70% effective transfer can provide roughly 63,000 BTU/h of useful heating under representative conditions. However, that figure should not be treated as a guaranteed field value. Actual performance depends on gas type, injector selection, air-fuel ratio, pan construction, grate geometry, kitchen ventilation, and operator settings.
Why pan diameter changes the required burner power
Pan diameter directly affects how burner energy is distributed. When the burner is too small for a large pan, the center becomes excessively hot while the outer cooking area remains comparatively cool. When the burner is too large for a small pan, flames may extend around the cookware, increasing radiant losses and heating the surrounding work area.
This relationship is particularly important when customers search for solutions using terms such as restaurant stove BTU pan size. A useful specification should therefore describe burner output together with the intended pan diameter rather than presenting BTU as an isolated number.
- 180–240 mm pans: approximately 25,000–50,000 BTU/h for standard cooking tasks.
- 240–320 mm pans: approximately 40,000–75,000 BTU/h for sautéing, boiling, and general restaurant production.
- 300–400 mm pans: approximately 60,000–100,000 BTU/h for high-volume cooking.
- 400–500 mm heavy cookware: approximately 80,000–130,000 BTU/h where rapid recovery is required.
These ranges are engineering starting points rather than universal prescriptions. A professional Manufacturer evaluates the complete cooking process, including the mass of food, initial food temperature, required recovery time, cookware material, and expected duty cycle.
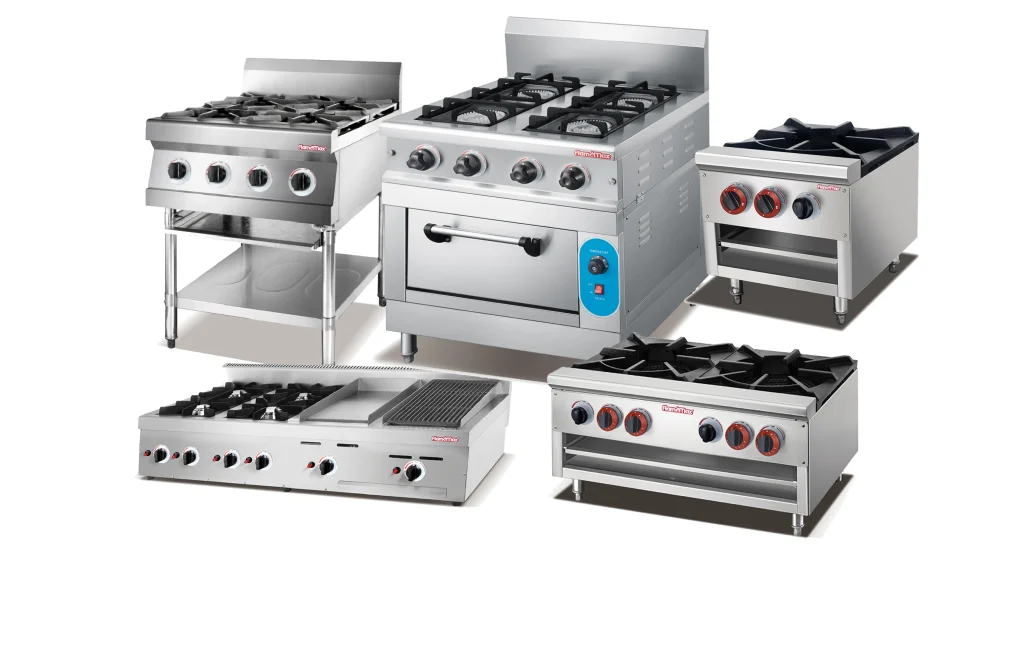
Account for pan material and bottom construction
Pan material changes the way available energy is distributed. Aluminum responds quickly because of its high thermal conductivity, while cast iron has greater thermal mass and can retain heat for longer periods. Stainless steel offers durability and corrosion resistance but generally benefits from an aluminum or copper core when rapid heat distribution is required.
For importers and commercial kitchen distributors, this means the same burner specification may produce different user experiences depending on the cookware supplied with the equipment. An OEM project for a hotel chain may therefore require a different burner configuration from an ODM project for a fast-food operation, even when the nominal pan diameter is similar.
| Application | Typical Pan Diameter | Typical Burner Input | Priority | Recommended Heat Behavior |
|---|---|---|---|---|
| Sauce and light cooking | 180–240 mm | 25,000–50,000 BTU/h | Control | Stable low flame and rapid adjustment |
| Restaurant sautéing | 240–320 mm | 40,000–75,000 BTU/h | Balance | Even heating with moderate recovery |
| High-volume boiling | 300–400 mm | 60,000–100,000 BTU/h | Recovery | Strong concentrated heating |
| Large stockpot production | 400–500 mm | 80,000–130,000 BTU/h | Power | High sustained heat transfer |
The table demonstrates why a simple “higher BTU is better” approach is unsuitable. The correct burner is the one that provides the required useful energy across the intended cookware area without creating excessive localized heating or unnecessary energy loss.
Estimate restaurant stove BTU pan size from the actual workload
A professional specification should start with the cooking task rather than the burner itself. Consider a restaurant boiling 20 liters of water. The required burner power depends on the starting temperature, desired boiling time, vessel efficiency, heat losses, and frequency of repeated batches. A hotel breakfast kitchen operating continuously has a different requirement from a small restaurant preparing occasional sauces.
For practical project estimation, the purchasing team can collect:
- Maximum liquid or food batch size in kilograms or liters.
- Target heating time and required recovery time.
- Pan diameter and bottom contact area.
- Pan material and approximate wall or bottom thickness.
- Daily operating hours and peak cooking periods.
- Available gas type and nominal supply pressure.
- Local installation requirements and ventilation capacity.
For example, a 30-liter stockpot used repeatedly during a lunch rush may need substantially greater recovery capacity than a 10-liter pot used intermittently. The correct commercial range burner power therefore depends on process throughput as much as cookware dimensions.
Why gas burner heat transfer matters more than nominal BTU
BTU input describes how much fuel energy enters the burner system; it does not directly describe cooking performance. Two burners with the same rated input can behave differently because of burner-head design, port geometry, flame velocity, mixing quality, grate height, and pan-to-flame distance.
A high-quality Supplier should evaluate the entire heat path. In a correctly engineered configuration, the flame should remain stable over the intended operating range while directing a substantial portion of combustion energy toward the pan base. Excessive flame lift, yellow flame, impingement on the pan edge, or unstable combustion can reduce effective performance.
In demanding installations, engineers should also consider continuous-duty operation, high kitchen ambient temperature, restricted ventilation conditions, and frequent burner cycling. These environmental factors influence both perceived performance and component durability.
- Verify flame stability at minimum, medium, and maximum settings.
- Check combustion behavior after extended operation.
- Measure pan-side temperature distribution rather than relying only on flame appearance.
- Confirm that burner components remain within their intended temperature range.
- Evaluate recovery time using the actual cookware and representative food load.
Match the burner system to electrical and gas infrastructure
Modern commercial cooking equipment is rarely an isolated gas appliance. Many ranges incorporate ignition systems, safety valves, flame-failure protection, electronic controls, thermostatic functions, or indicator systems. Therefore, the gas supply network and electrical control circuit should be treated as part of the same system topology.
For projects using electronic ignition, the engineering team should confirm the available 220–240 V single-phase electrical supply, frequency, grounding method, protection device, and control architecture. Export projects may instead require adaptation to 110–120 V electrical environments. At the same time, the gas side may use LPG or natural gas with different supply pressures and injector requirements.
A representative system topology can be described as:
- Building gas supply → isolation valve → pressure regulation → manifold → individual burner valves → burner heads.
- Electrical supply → protective device → ignition/control module → ignition electrode and safety monitoring system.
- Kitchen exhaust system → canopy → grease filtration → ventilation duct → external discharge.
For overseas OEM programs, a Manufacturer should verify these interfaces before production. A Customizable control panel, logo, gas configuration, electrical specification, or safety component can then be incorporated into the equipment according to the project requirements.
Control environmental challenges in commercial kitchens
Commercial kitchens create an unusually demanding environment for cooking equipment. Heat, steam, grease, cleaning chemicals, vibration, and long operating cycles can affect ignition components, wiring, valves, surface finishes, and control systems. Coastal markets can introduce additional concerns because high humidity and salt-laden air may accelerate corrosion on exposed metal components.
Equipment installed in busy hotel kitchens may also operate close to other high-temperature appliances. The surrounding air temperature can rise substantially during peak service, while the exhaust system continuously changes the pressure and airflow around the burner.
- Use heat-resistant electrical wires and components suitable for the operating environment.
- Protect electrical connections from direct exposure to water and cleaning chemicals.
- Use appropriate stainless-steel grades and surface treatments for demanding environments.
- Maintain adequate clearance around combustion and ventilation components.
- Check ignition reliability after repeated hot-start cycles.
- Consider local gas regulations before finalizing injector and valve specifications.
These details are especially important for distributors supplying multiple countries. A standard product may require a Customizable configuration to meet local utility conditions while preserving the same basic cooking platform.
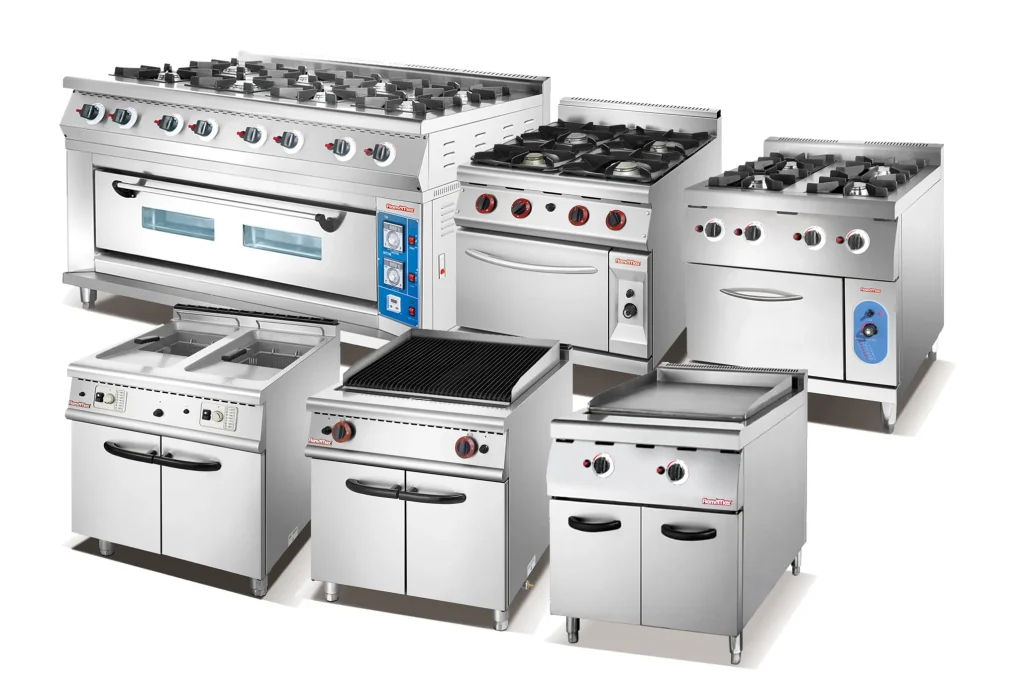
Why representative performance testing is essential
Laboratory specifications provide useful reference information, but commercial cooking equipment should also be tested under realistic operating conditions. A representative performance test should reproduce the cookware size, food or water load, gas pressure, electrical supply, and duty cycle expected in the customer’s kitchen.
For a burner evaluation, engineers can record:
- Time required to heat a defined water mass from a specified starting temperature.
- Recovery time after adding a controlled cold load.
- Flame stability at low, medium, and maximum settings.
- Pan-bottom temperature distribution at defined measurement points.
- Gas consumption over a representative operating period.
- Electrical ignition reliability across repeated start cycles.
- Surface temperature around the control and operator interface.
This approach helps distinguish theoretical burner capacity from practical cooking performance. It is also valuable for OEM and ODM customers because the test procedure can become part of the product acceptance standard for repeated production batches.
Create a representative performance test
A practical test can use a standardized stainless-steel or aluminum vessel filled with a defined water quantity. For example, a 300 mm pan may be filled with 10 liters of water and operated at the intended maximum burner setting. The test should record starting temperature, ambient temperature, gas pressure, burner input, heating time, and pan-side temperature.
For a high-output 80,000 BTU/h configuration, the engineering team may establish a target heating curve rather than relying on a single final temperature. This makes it easier to identify unstable combustion, poor flame distribution, or excessive heat concentration. If the customer requires rapid batch recovery, the test should also include repeated cold-load additions.
The test environment should document ambient temperature, relative humidity, gas supply pressure, electrical voltage, and ventilation operating status. Recording these parameters creates a reproducible engineering baseline.
For international supply projects, the test report can also identify the selected injector, valve type, burner diameter, grate height, electrical configuration, and safety system. This reduces ambiguity between the customer’s purchase specification and the final production configuration.
Design for OEM and ODM commercial kitchen projects
Large distributors and hotel-equipment purchasers often require more than an off-the-shelf burner. They may need a specific burner arrangement, control layout, brand identity, carton design, panel appearance, or gas/electrical configuration. In these projects, OEM and ODM engineering should begin with application requirements instead of cosmetic changes.
A capable Manufacturer and Supplier can structure the project around several levels of customization:
- Burner diameter and output selection.
- Natural gas or LPG configuration.
- Injector and valve specification.
- Pan-support and grate geometry.
- Ignition and flame-failure protection.
- Control-panel layout and labeling.
- Logo, color, carton, and product identification.
- Electrical configuration for different export markets.
For a distributor developing a private-label commercial range, ODM support can also include performance optimization around a specified cookware family. This provides a more application-focused solution than simply selecting the highest-output burner available.
Why application-based selection improves commercial reliability
The main engineering objective is not maximum burner power; it is controlled energy delivery that matches the cookware and cooking process. Correct matching improves recovery, temperature consistency, operator comfort, energy utilization, and equipment durability.
For importers and wholesalers, this application-based method also simplifies product positioning. Instead of offering customers several burners distinguished only by BTU ratings, the Supplier can classify products by cooking task, pan diameter, batch size, and expected operating intensity.
FLAMEMAX operates as a professional commercial catering equipment Manufacturer with a large production facility, advanced processing equipment, structured testing procedures, and experience serving international B2B customers. Its production approach includes full product inspection before packing, flexible customization, OEM and ODM support, and technical assistance for overseas projects.
Summary for commercial range burner selection
Proper burner selection requires matching commercial range burner power, pan diameter, cookware material, gas conditions, electrical environment, ventilation, and workload. Importers and distributors can send their pan size, batch capacity, gas type, electrical specification, and target cooking time to FLAMEMAX for an application-focused solution and quotation.

 English
 Español
 Français
 Italiano
 日本語
 Deutsch
 Русский
 한국어
 简体中文